

Blogs
May 6, 2026

A packaging line rarely underperforms because robotic equipment lacks speed. In most cases, inefficiencies arise when release, accumulation, and transfer logic are treated as secondary considerations. […]
April 28, 2026

Material handling systems play a critical role in production efficiency, product quality, and operational continuity. Selecting the right industrial conveyor manufacturer is not simply a procurement […]
April 28, 2026
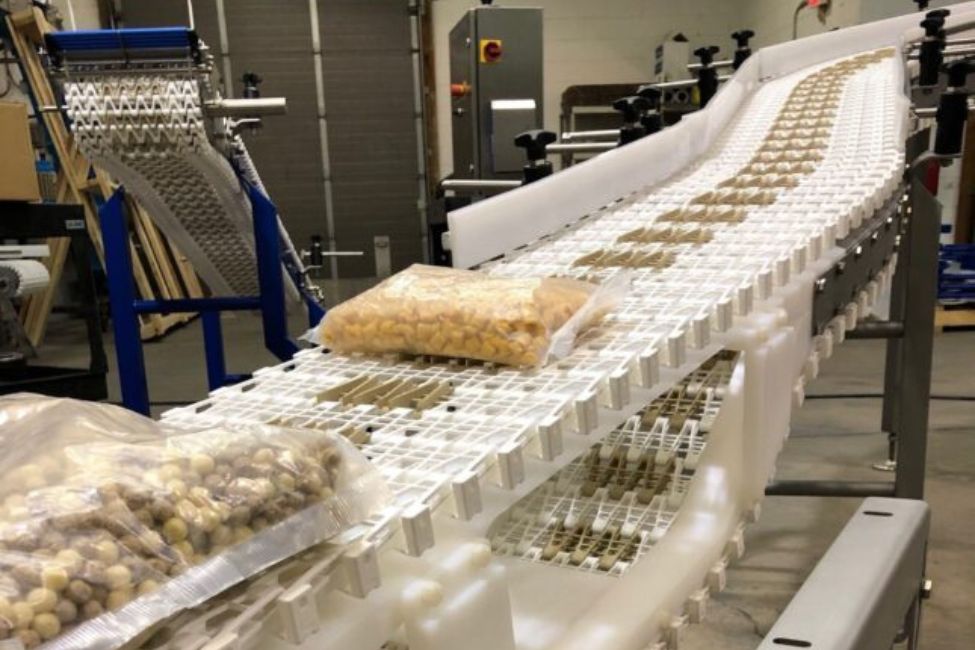
Food safety has become a defining factor in modern processing facilities, where even minor contamination risks can disrupt operations and impact product quality. Leading food conveyor […]
April 28, 2026
Food manufacturing environments demand precision, hygiene, and consistent throughput across every stage of production. Conveyor systems play a central role in ensuring smooth product movement while […]
April 9, 2026

Industrial operations depend on conveyor systems that run consistently under demanding conditions. Even minor component failures can lead to downtime, reduced productivity, and increased operational costs. […]
April 6, 2026

Production environments that handle continuous product flow require systems that manage spacing, buffering, and product control without interrupting operations. An accumulation conveyor plays a critical role […]
April 2, 2026

Large-scale industrial projects demand more than standard equipment supply. Facilities handling high production volumes require conveyor systems that operate reliably across complex layouts and continuous operating […]
March 13, 2026

Material handling systems operate continuously across manufacturing, packaging, and distribution environments. These systems must maintain consistent product flow while supporting high production volumes and demanding operational […]
March 11, 2026

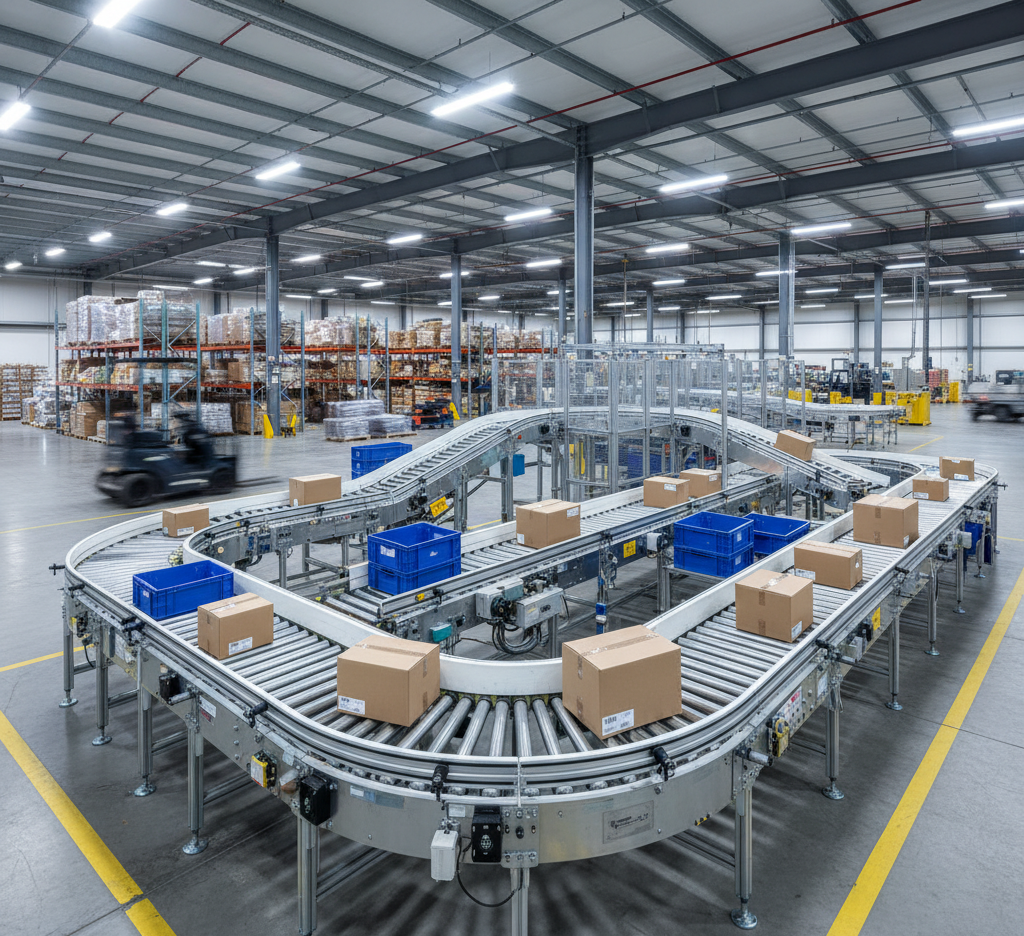
Industrial conveyor systems operate at the center of manufacturing, packaging, and distribution facilities. Reliability, safety, and operational consistency often depend on the standards followed during design […]